Ceramic Valve Solutions for TiO2 Crystallization and Thickening
Reliable isolation and discharge control for acidic titanium liquor containing abrasive and scaling ferrous sulfate crystals
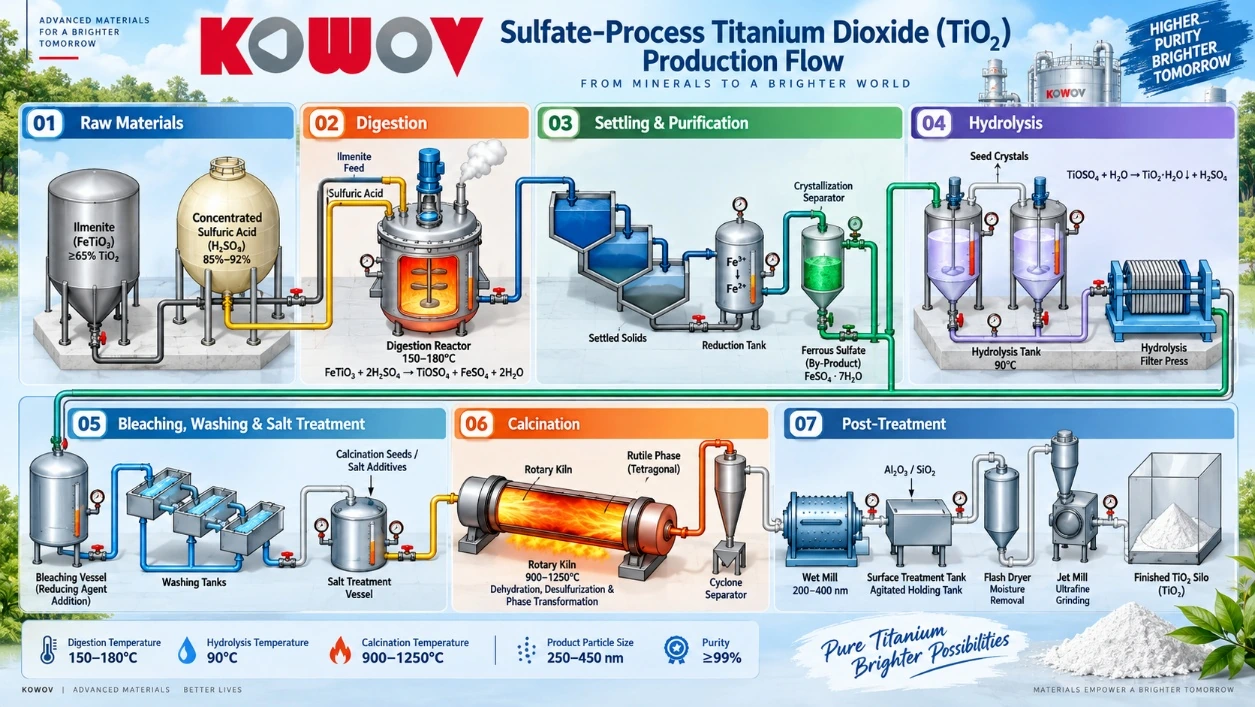
Crystallization Thickener
The crystallization thickener is a key piece of equipment connecting the crystallization stage with the solid-liquid separation stage in titanium dioxide production
It is mainly used in the sulfate-process TiO₂ production line, where it is installed downstream of the crystallizer, or vacuum flash crystallization system, and upstream of the centrifuge or filter
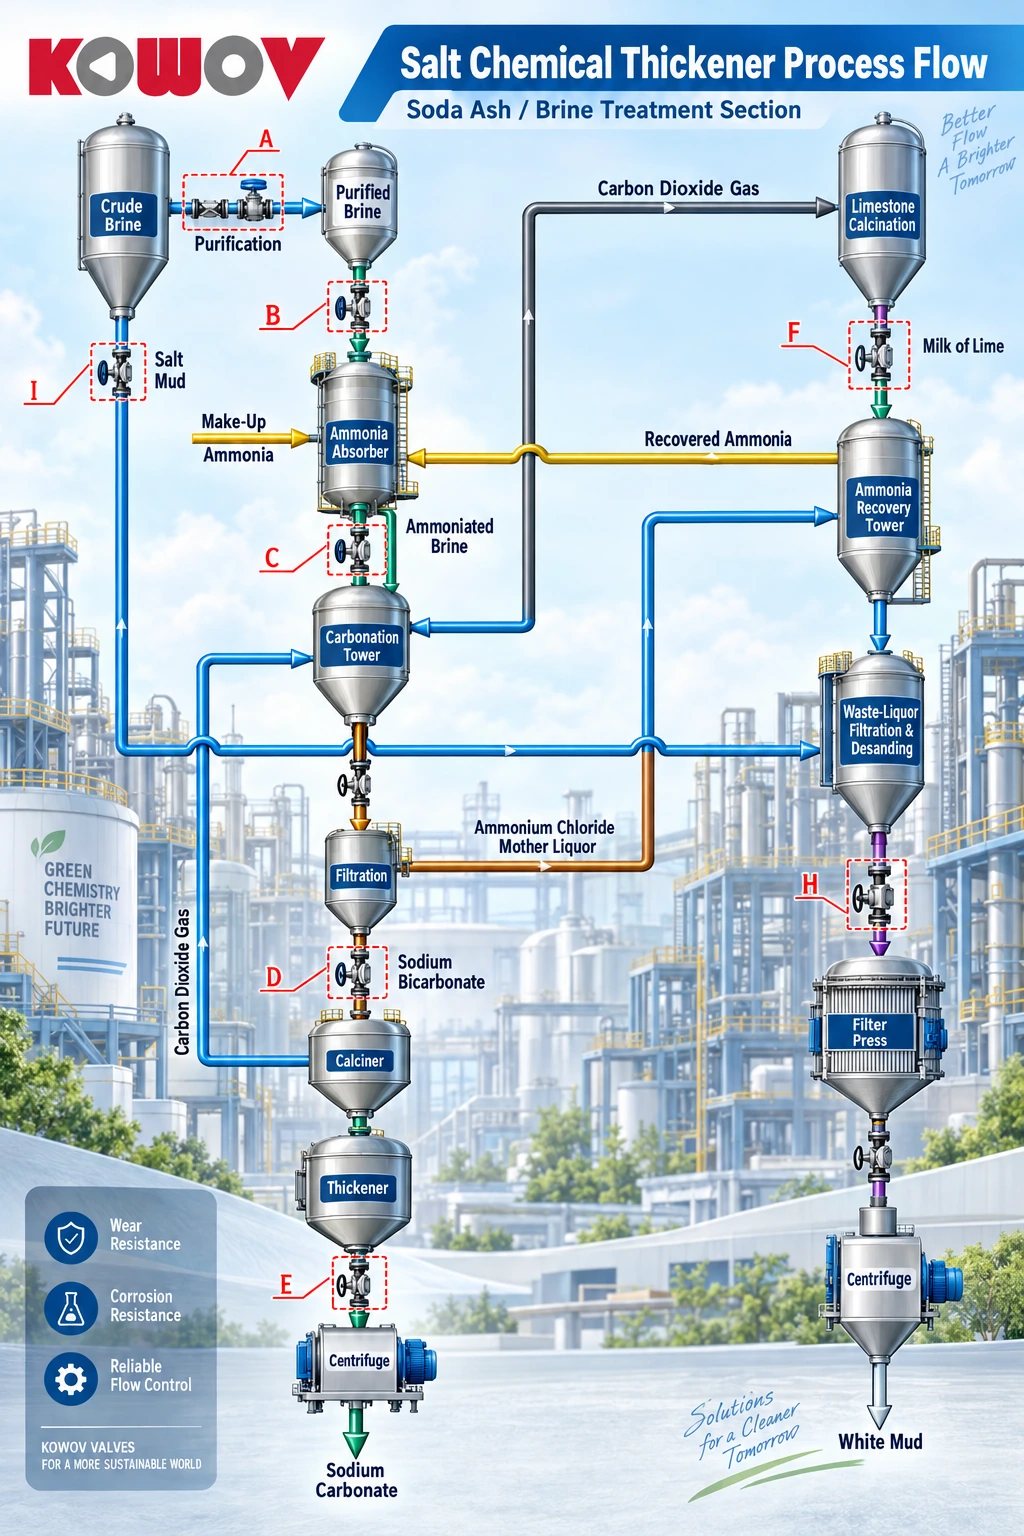
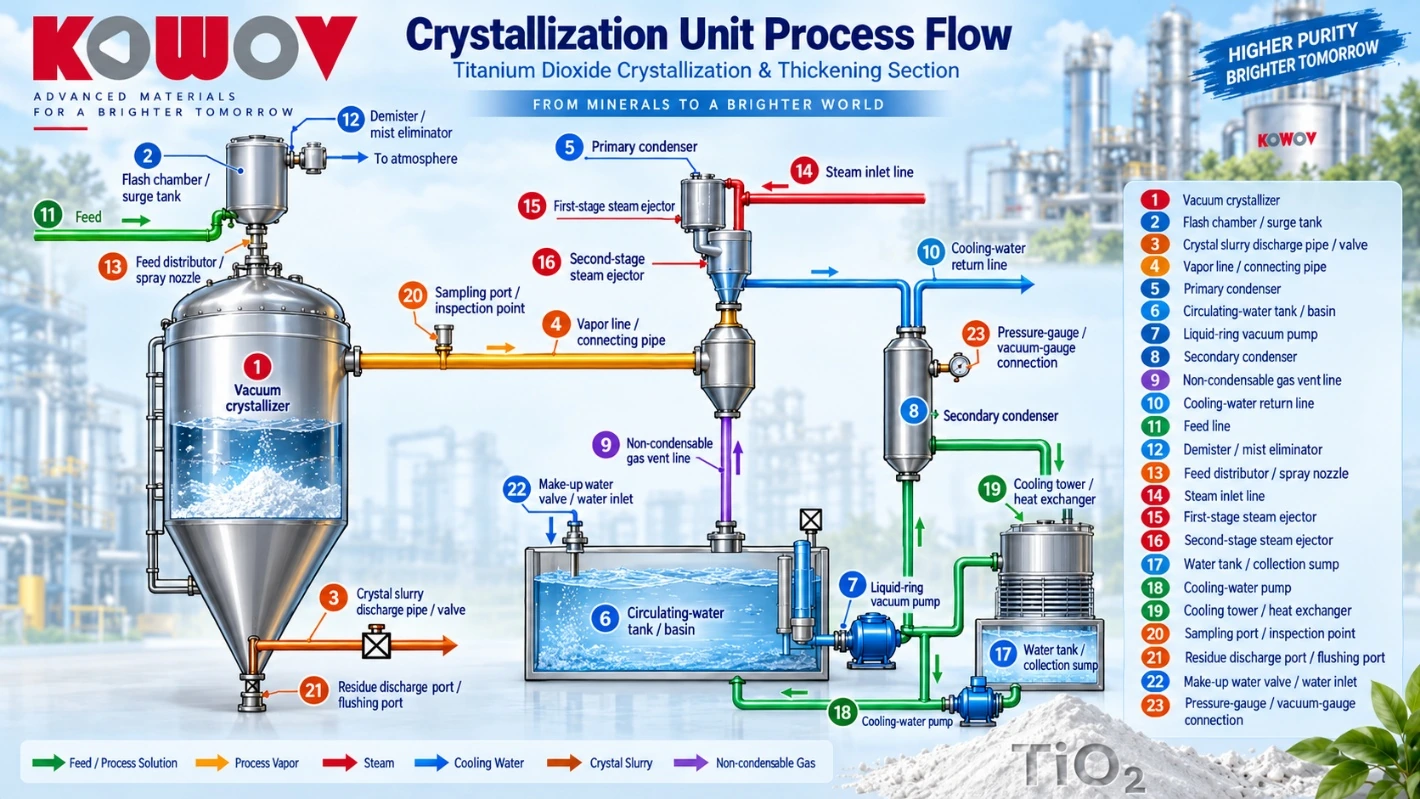
Crystallization unit process flow
Operating Conditions
Although the thickener has a relatively simple structure, it plays a critical role in the entire sulfate-process titanium dioxide production line. It directly determines the concentration and crystal size of the slurry entering the centrifuge, thereby affecting the separation efficiency of ferrous sulfate crystals, the ferrous sulfate recovery rate, and the iron content of the final product
| Item | Value | Rating / State | Characteristics |
|---|---|---|---|
| Medium | Crystal slurry | Solid-liquid two-phase | Corrosive and abrasive |
| Operating Pressure | 6-16 bar | Pressure Rating | Class 150 / PN16 |
| Differential Pressure (ΔP) | ≤6 bar | Nominal Size | DN25-DN250 |
| Operating Temperature | <100°C | - | No thermal shock |
| Parameter | Description |
|---|---|
| Chemical Composition | Strongly acidic titanium-bearing solution containing free sulfuric acid |
| Corrosive Component | Sulfuric acid |
| Corrosiveness (pH) | pH 1-2 |
| Solid Content | Solid particles: FeSO₄·7H₂O crystals |
| Particle Size | D50 >15 μm |
| Particle Hardness | Mohs hardness: approximately 5.5-6.0 |
Special Operating Conditions
Chemical Corrosion
In crystal slurry service, crystals precipitate and adhere to low-velocity areas such as valve sealing surfaces and cavity dead zones, creating concentration-gradient cells. Corrosion begins at microscopic defects in the sealing surface. Although initially difficult to detect, it develops rapidly once initiated
Physical Abrasion
Precipitated crystals, including FeSO₄·7H₂O, Na₂SO₄, and urea crystals, are extremely hard despite their microscopic size. As they continuously flow through the valve, they scour the sealing surfaces and flow-passage walls, causing low-stress abrasive wear
Wear becomes particularly severe at throttling points, where the sharply increased velocity and particle kinetic energy significantly intensify erosion
Severe Interaction Between Viscosity and Crystallization
High viscosity reduces flow velocity, while lower velocity increases material residence time. Longer residence time promotes further crystal precipitation, increasing the slurry viscosity even more
This creates a destructive cycle
Higher viscosity → Lower flow velocity → Increased crystallization → Further viscosity increase
Ultimately, the valve and pipeline may become completely blocked
Synergistic Acceleration of Corrosion and Wear
Corrosion weakens the mechanical properties of the base material, making it more vulnerable to crystal-particle erosion. Abrasion then removes the corrosion-resistant surface layer, such as a passivation film or coating, and exposes fresh metal to the corrosive medium
This results in a synergistic effect of corrosion-accelerated wear and wear-accelerated corrosion, reducing actual valve life far below the expected life calculated from corrosion or wear alone
Equipment Hazards
Corrosion, abrasion, crystal blockage, and viscosity fluctuations do not occur independently. Together, they form a triple-coupled destructive cycle of crystallization-corrosion-abrasion, making valve failure mechanisms far more complex than damage caused by corrosion or wear alone
Engineering hazard: At locations with stagnant flow, leaking valves, or inadequate anti-corrosion coatings, crystals can form dense, hard scale layers. These deposits may sharply reduce the effective pipeline diameter or cause complete blockage. Expansion stresses generated during crystallization can also crack and detach protective coatings, compromising equipment sealing integrity
Keywords: Sulfate Process · Crystal Slurry · Crystallizer · Thickener · Sedimentation and Crystallization · Thickened Slurry · Slurry Conveying
Process Pain Points and Key Opportunities
Existing Valve Materials and Types
Valves commonly used on site include
- Gate valves made of cast iron, HT200 grey cast iron, or WCB cast steel
- Metal-seated ball valves and globe valves made of WCB cast steel
- Conventional rubber-lined gate valves and butterfly valves lined with natural rubber or hard rubber
Problems with Existing Valves
Material accumulation inside the valve cavity, stem seizure and difficult operation, wear-induced internal leakage, valve-body perforation, blocked flow passages, guide-component sticking or complete seizure, and external leakage of the process medium
Replacement Interval and Service Life
Valve service life is typically only about six months. Frequent failures in crystal-slurry service result in repeated inspection and replacement and high maintenance costs
Losses Caused by Unplanned Shutdowns
The most immediate consequences of an unplanned shutdown are production-line interruption and output dropping to zero. However, fixed costs, including labor, depreciation, energy, and other overheads, continue to accumulate
Restarting after a shutdown requires a controlled temperature increase and a thorough system inspection. When the equipment is restarted, it is subjected to considerable starting torque, which may overload the motor or damage the coupling
Unplanned shutdowns are often accompanied by loss of process control, creating a high-risk period for safety incidents
Valve sealing-surface damage, pipeline wear, and related failures also result in substantial maintenance expenses, including spare-parts procurement, labor, inspection, and outsourced services
Case Study
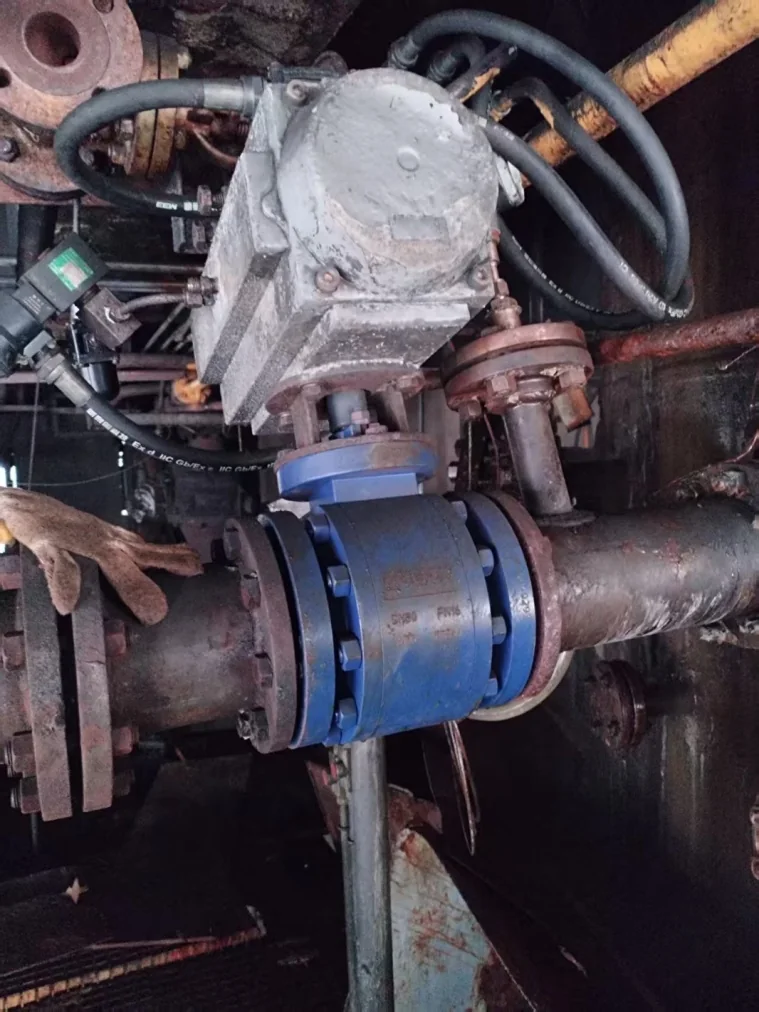
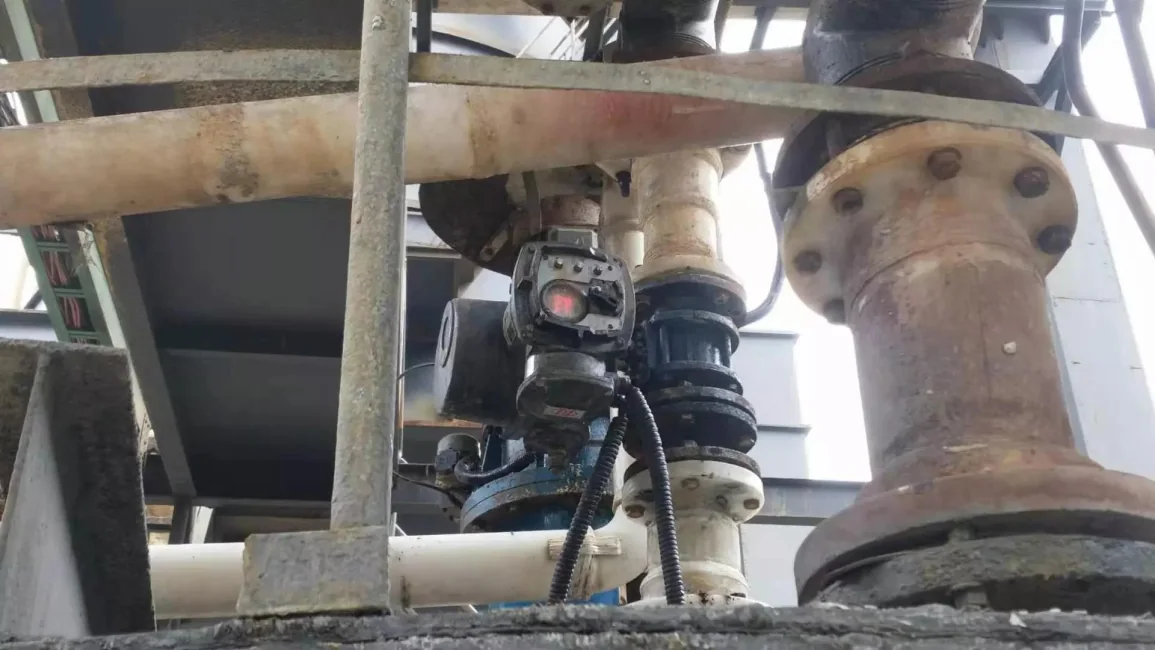
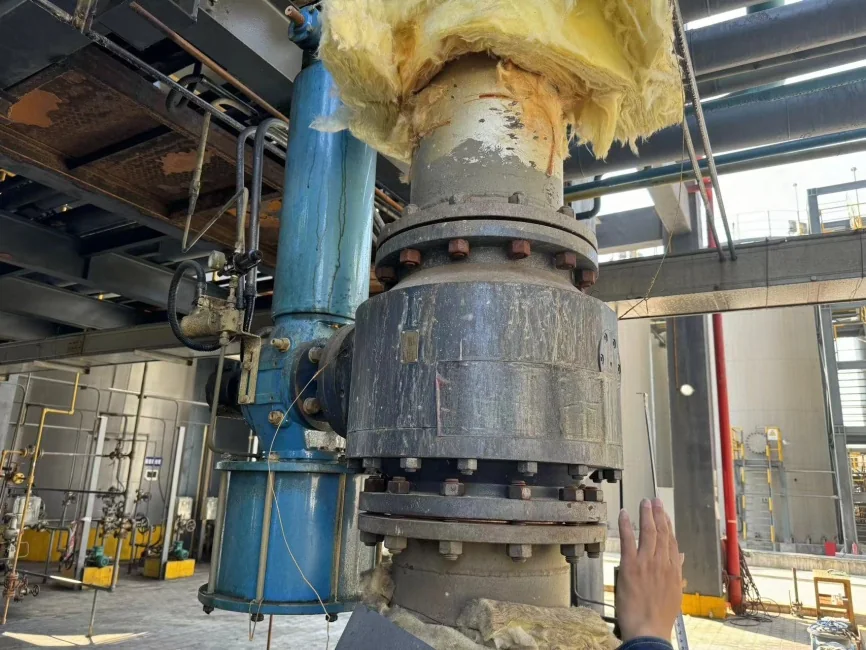
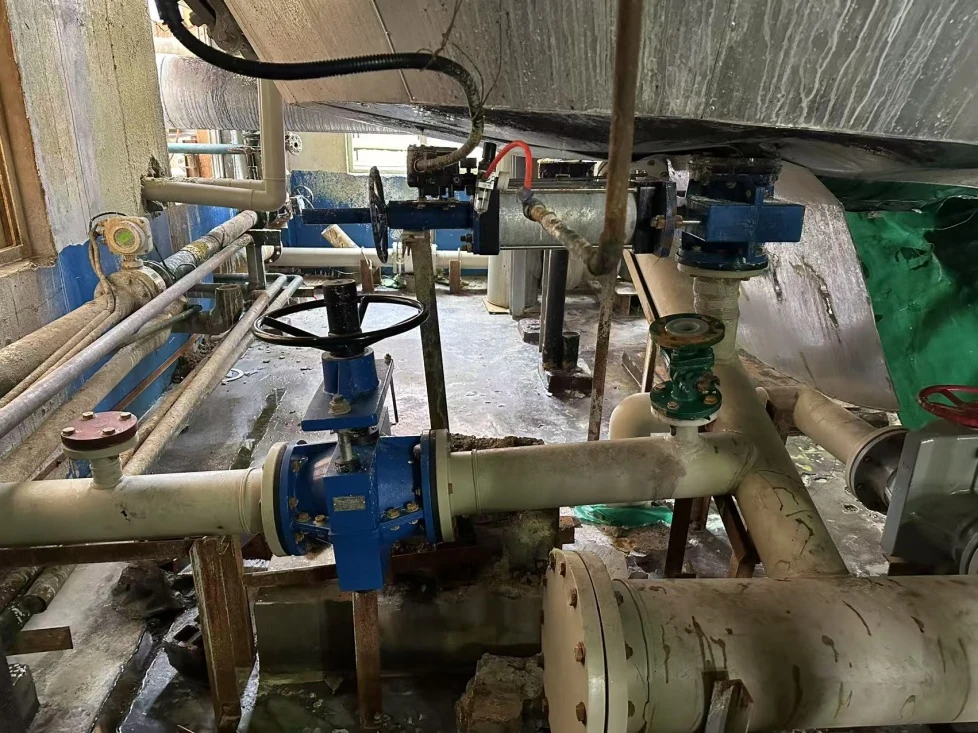
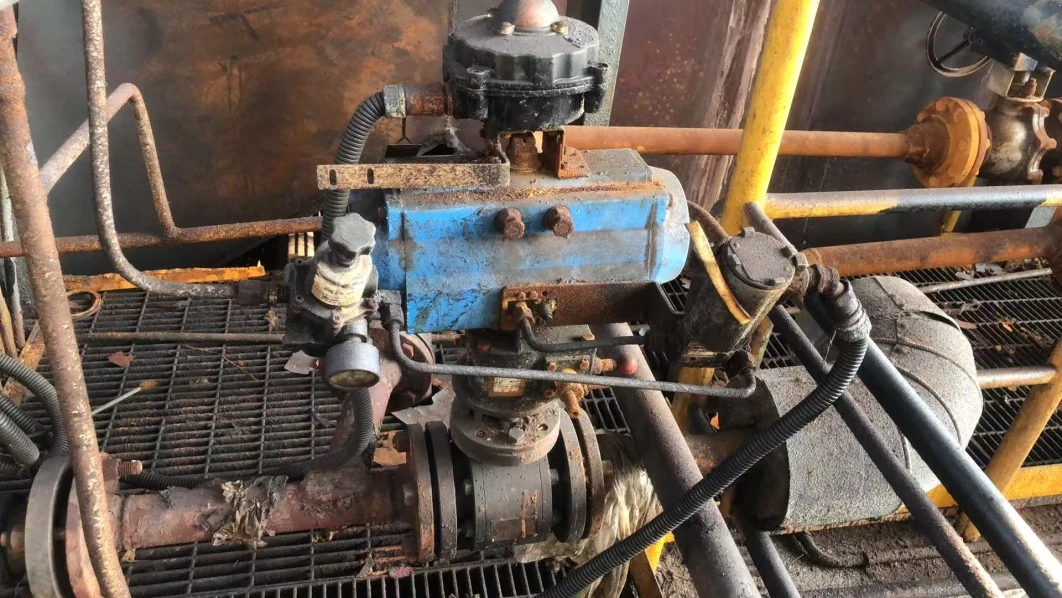
TiO2 Crystallization and Thickening: site photographs
End Users
- Sichuan Lomon Titanium Industry Co., Ltd., China, in service since 2019
- LB Sichuan Titanium Industry Co., Ltd., China, in service since 2020
In sulfate-process titanium dioxide production, the crystal thickener is a critical component of the iron-removal section. It is mainly used to efficiently separate and concentrate ferrous sulfate heptahydrate crystals precipitated from the titanium-bearing solution after vacuum or cooling crystallization
The medium handled by the crystal thickener is a titanium-bearing liquor containing ferrous sulfate crystals, a solid-liquid mixture formed after crystallization:
- Liquid phase: primarily titanyl sulfate solution
- Solid phase: FeSO₄·7H₂O crystals
- Crystal size: approximately 0.5-2 mm
- Crystal hardness: Mohs hardness of approximately 5
- Medium characteristics: strongly acidic, with a pH of approximately 1-2; highly viscous; prone to crystallization; extremely corrosive; and liable to crystal agglomeration and pipeline blockage
At one titanium dioxide plant, the original valves used in this section were fluoropolymer-lined butterfly valves or Hastelloy valves. Neither could simultaneously withstand both corrosion and abrasion. Frequent failures occurred due to corrosion of the sealing surfaces, abrasive wear, and crystal buildup inside the valve cavity. Valve service life was no more than six months
After replacement with KOWOV ceramic ball valves, on-site performance improved significantly. The valves have operated continuously and reliably for nearly four years, eliminating the need for frequent valve replacement
Conclusion
Minimum Service Life
- On/Off Valves: ≥3 years
- Control Valves: ≥2 years
Why Choose Ceramic Valves?
Superior Wear Resistance
Structural ceramics have a Rockwell hardness of over HRA 87. Their wear resistance is approximately 266 times that of manganese steel and 172 times that of high-chromium cast iron, far exceeding that of conventional metals and fluoropolymer-lined valves
They withstand continuous erosion and abrasion, helping prevent internal leakage and significantly reducing valve replacement frequency
Excellent Corrosion Resistance
Structural ceramics are inorganic, non-metallic materials with exceptional chemical stability. They resist corrosion from acids, alkalis, and salts, making them suitable for most corrosive acid-alkali media encountered in salt-chemical processes
Smooth Surface and Low Adhesion
Structural ceramics feature self-lubricating and self-cleaning surfaces that effectively prevent material adhesion and accumulation
With a hardness of up to HRA 90, they withstand continuous particle erosion while ensuring precise feed-flow control
Improved Process Quality
The high mechanical strength and smooth surface of sintered ceramics reduce the adhesion and accumulation of aluminum and sodium salt crystals. The valve trim resists erosion and material buildup, while its precision sealing surfaces prevent internal leakage and cross-contamination
This helps maintain reliable sealing and improve product consistency between pharmaceutical batches
Conclusion
Ceramic ball valves and ceramic C-port valves support the safe, stable, and long-term operation of salt-chemical production lines, significantly reducing shutdowns and maintenance requirements
Commonly Used Products
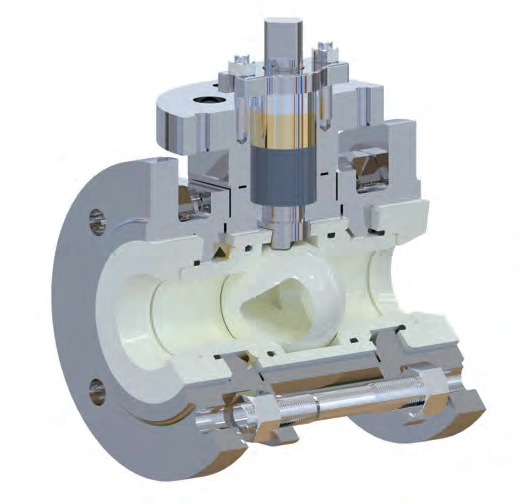
FCCV1
Standard Ceramic Ball Valve
A standard ceramic ball valve featuring a proven, versatile design. It is suitable for both on/off and modulating service and can handle operating temperatures up to 180°C and pressures up to 5.0 MPa
Its ceramic-to-ceramic sealing structure delivers excellent sealing performance, with particularly reliable shut-off in applications containing solid particles
- Size range: DN15-250 (½″-10″)
- Leakage Class: Class IV or higher
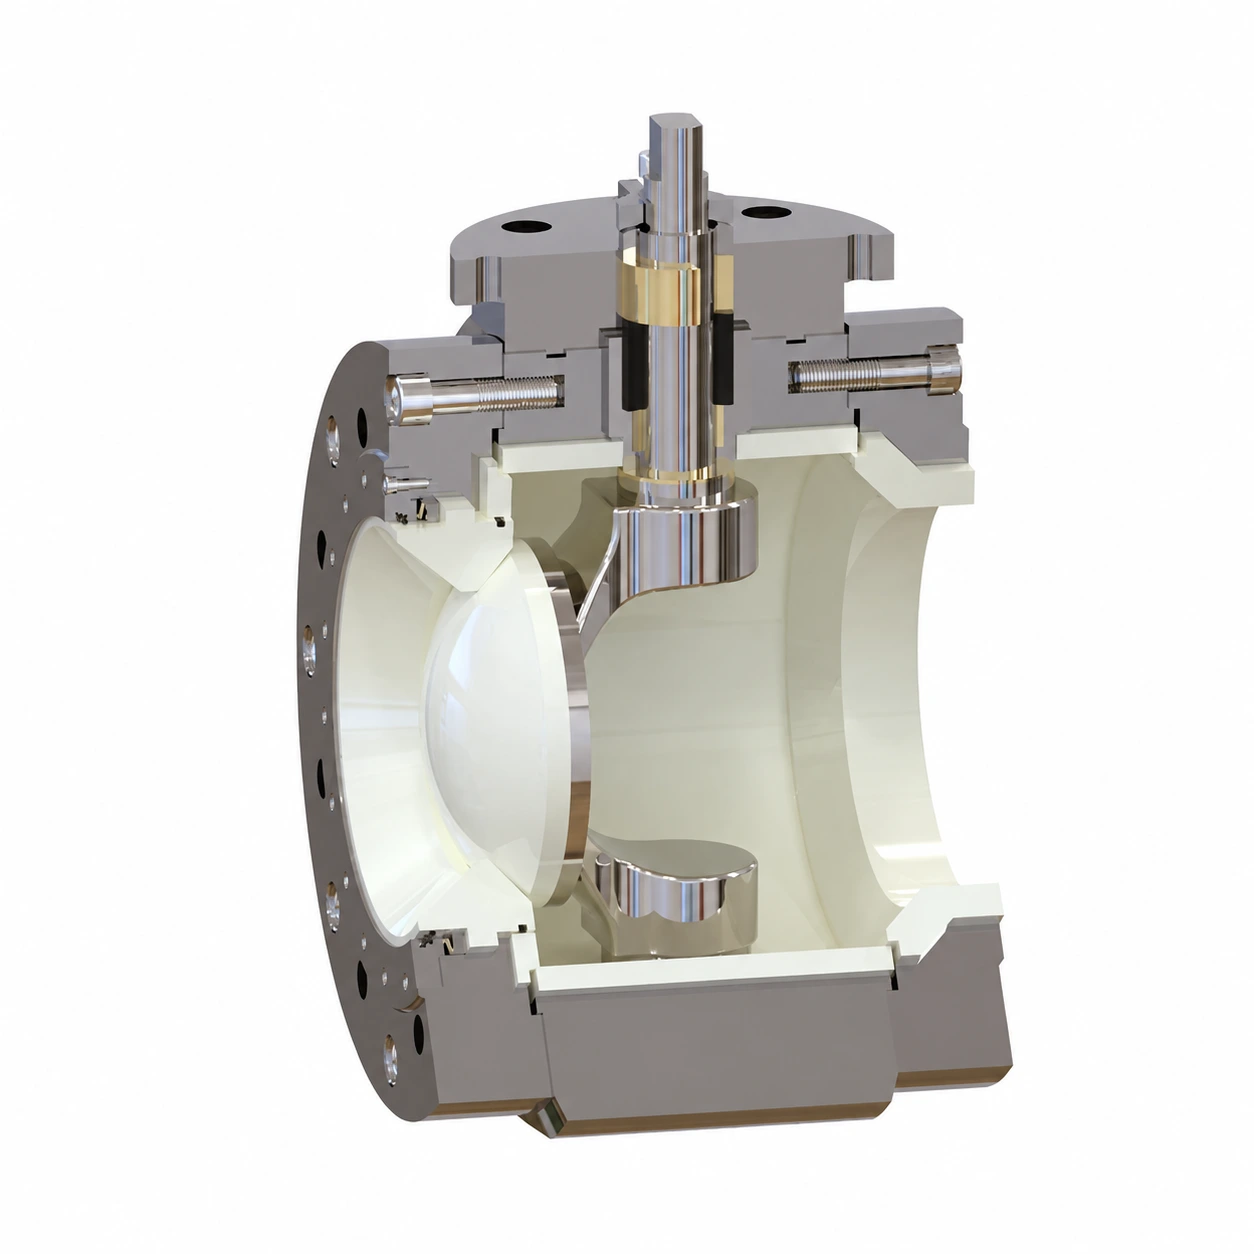
FCRV
Ceramic C-Port Rotary Valve
This valve features a patented C-port design. The ceramic ball segment consists of a C-shaped support and a ceramic spherical crown joined through a mechanical interlocking connection. The spherical crown is manufactured as an integral ceramic component, protecting the C-shaped support from direct erosion by the medium
The valve incorporates an eccentric design. During opening and closing, the ceramic spherical crown remains in close contact with the seat, scraping away adhesive deposits from the sealing surfaces and ensuring reliable sealing performance
It is particularly suitable for media prone to adhesion, scaling, crystallization, high solids content, and sedimentation. Its cavity-free flow path prevents material accumulation inside the valve body
Size range: DN50-400
View FCRV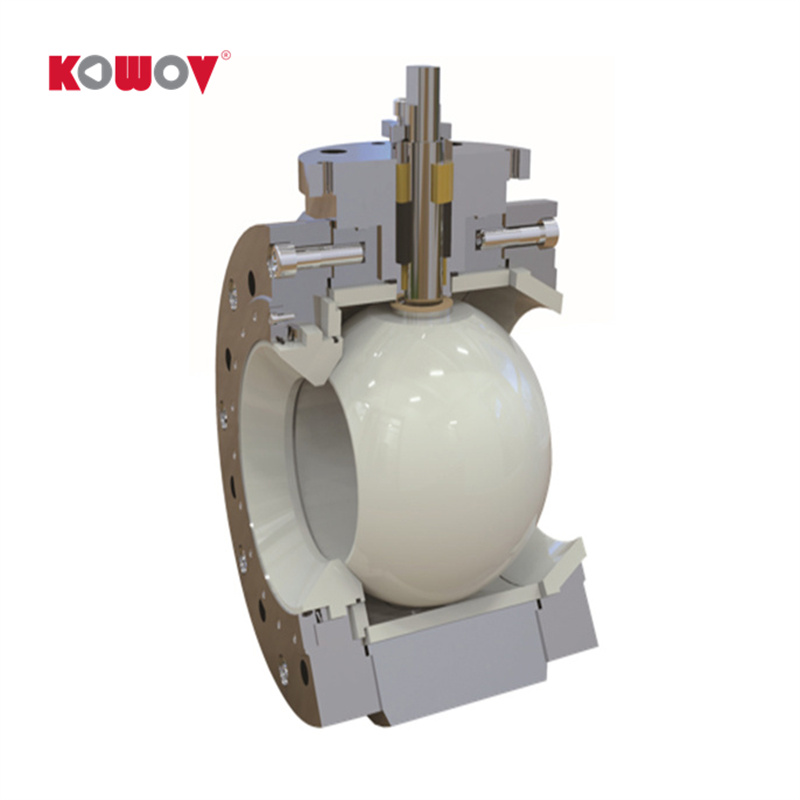
FCCV6
Single-Seat Ceramic Ball Valve
This cavity-free ceramic ball valve is designed for highly adhesive, crystallizing, scaling, and mineral-slurry applications
Its robust construction provides reliable, long-term performance and prevents material from entering and accumulating inside the valve cavity. Each opening and closing cycle allows the ceramic ball to scrape deposits from the sealing surfaces, helping maintain cleanliness and reliable shut-off
Size range: DN25-400
View FCCV6Contact Us
Talk to our team about your TiO2 crystallization and thickening application
Discuss your application